Waterproof Breathable Membrane Factory Solutions

waterproof breathable membrane factory

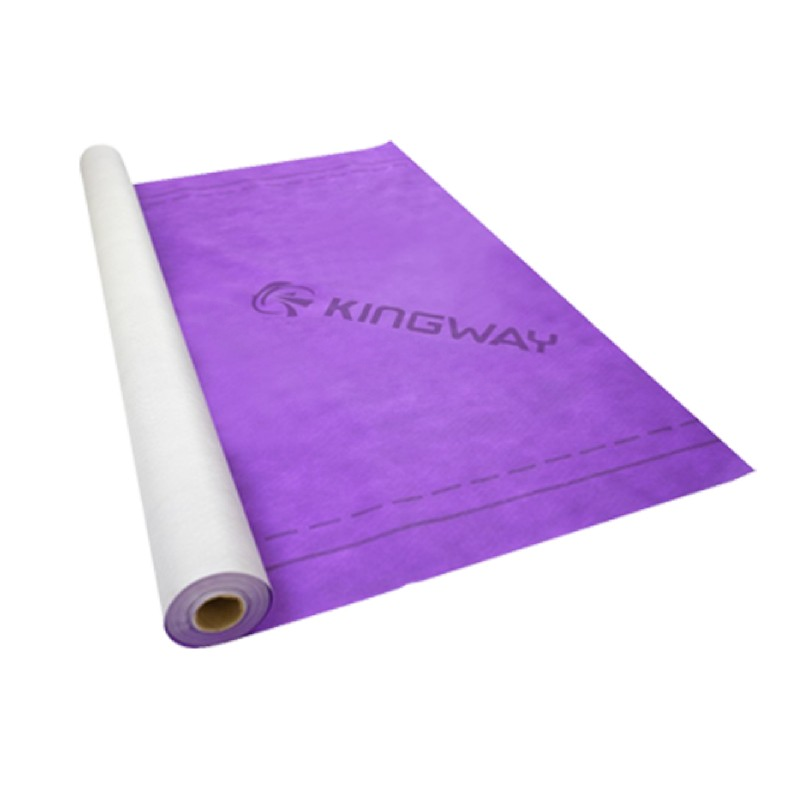
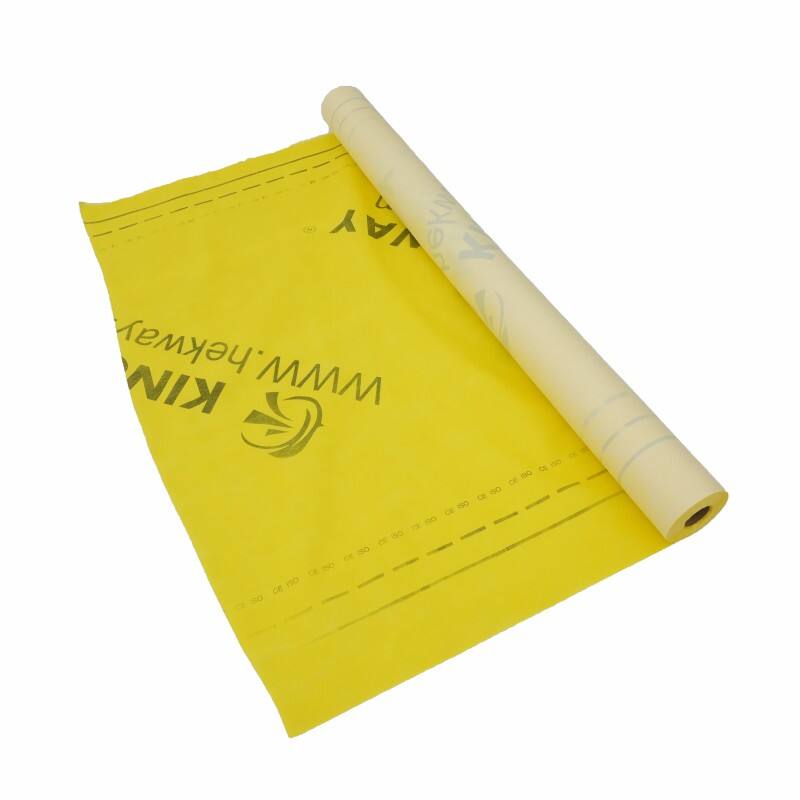
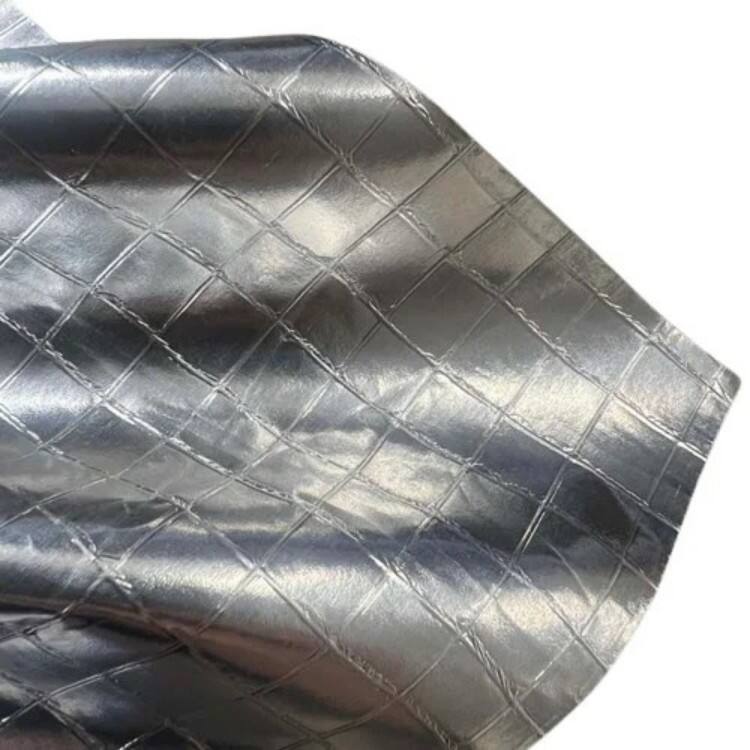
A waterproof breathable membrane factory specializes in manufacturing advanced protective materials that simultaneously prevent water penetration while allowing vapor transmission. These facilities produce technical textiles engineered with microscopic pore structures that block liquid water molecules but permit smaller water vapor molecules to pass through. Modern waterproof breathable membrane factory operations integrate sophisticated polymer science, precision coating technologies, and quality control systems to deliver consistent high-performance products. The main functions include producing membranes for construction, apparel, medical, and industrial applications through processes like laminating, coating, and bonding. Technological features encompass microporous structures, hydrophilic coatings, multi-layer constructions, and specialized polymer formulations that achieve optimal waterproof ratings while maintaining breathability. A professional waterproof breathable membrane factory employs automated production lines with climate-controlled environments to ensure dimensional stability and performance consistency. Applications span roofing underlayment, wall systems, outdoor sportswear, footwear, medical garments, filtration systems, and protective equipment. The manufacturing process typically involves substrate preparation, polymer application, curing, lamination, quality testing, and finishing. Advanced facilities utilize electron microscopy, hydrostatic pressure testing, and moisture vapor transmission rate analysis to verify product specifications meet international standards including ISO, ASTM, and EN certifications for various end-use requirements across diverse markets.
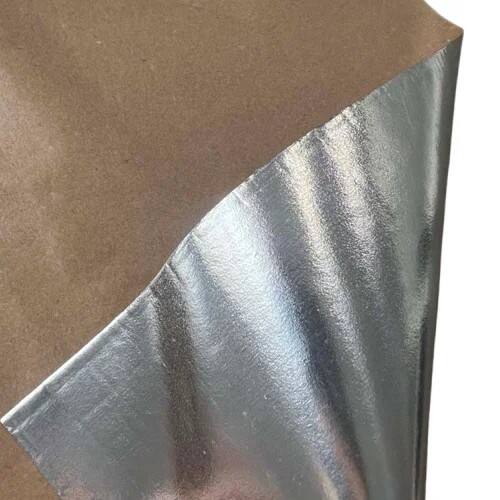
Popular Products

Choosing a reliable waterproof breathable membrane factory delivers substantial practical benefits that directly impact your product quality and business success. First, you gain access to consistent material performance through controlled manufacturing environments that eliminate variables affecting membrane properties. This consistency means your products perform predictably across different batches, reducing customer complaints and warranty claims. Second, established factories offer customization capabilities tailored to your specific application requirements, whether you need particular waterproof ratings, breathability levels, or physical properties like tear strength and flexibility. This customization eliminates the compromise of using generic materials that may not perfectly suit your needs. Third, working directly with a waterproof breathable membrane factory typically provides better pricing than purchasing through distributors, improving your profit margins while maintaining quality standards. Fourth, technical support from factory engineers helps you optimize material selection and application methods, preventing costly mistakes during product development. Fifth, reliable factories maintain quality certifications and testing documentation that simplify your compliance processes when entering regulated markets or meeting customer specifications. Sixth, production scalability allows you to start with small orders and increase volumes as your business grows without changing suppliers or reformulating products. Seventh, shorter lead times from factory-direct relationships accelerate your time-to-market compared to multi-tier supply chains. Eighth, transparency in manufacturing processes enables you to verify ethical practices, environmental standards, and material traceability that increasingly matter to conscious consumers. These operational advantages translate into reduced development costs, faster market entry, improved product reliability, and stronger competitive positioning across your target segments.

Latest News

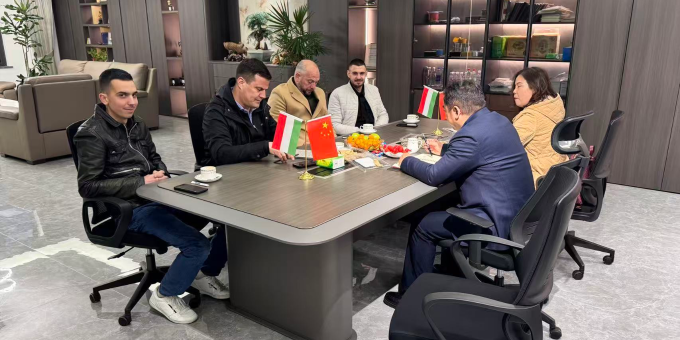
Hosting Important Clients from Europe.

08

Jan

Hosting Important Clients from Europe.

View More
A Heartwarming Moment for The New Members of Kingway

04

Jan

A Heartwarming Moment for The New Members of Kingway

View More
From Renting Factory Space to Becoming An Industry Benchmark: Kingway's Sixteen-year Journey of Excellence.

04

Jan

From Renting Factory Space to Becoming An Industry Benchmark: Kingway's Sixteen-year Journey of Excellence.

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

waterproof breathable membrane factory

Advanced Multi-Layer Manufacturing Technology

Advanced Multi-Layer Manufacturing Technology

A modern waterproof breathable membrane factory employs sophisticated multi-layer manufacturing technology that creates superior protective materials through precise engineering. This process begins with selecting appropriate substrate materials such as polyester or nylon fabrics, then applying polymer layers using controlled coating or lamination techniques. The factory utilizes specialized equipment that maintains exact temperature, pressure, and speed parameters to achieve uniform membrane thickness and consistent pore structures throughout every production run. Advanced quality control systems monitor critical properties at multiple production stages, using automated testing equipment to verify waterproof ratings, breathability measurements, adhesion strength, and physical durability. This technological approach ensures that every meter of membrane meets strict performance specifications, eliminating the inconsistencies common in less sophisticated manufacturing environments. The multi-layer construction allows factories to optimize different properties in each layer, combining waterproofing polymers with breathable layers and protective surfaces to create balanced performance profiles. This manufacturing sophistication directly benefits customers through reliable product performance, reduced failure rates, and confidence that materials will perform as specified across diverse environmental conditions and application stresses.
Comprehensive Application Engineering Support

Comprehensive Application Engineering Support

Distinguished waterproof breathable membrane factory operations provide comprehensive application engineering support that extends beyond simply selling materials. Expert technical teams work directly with customers to understand specific performance requirements, environmental challenges, and application methods relevant to their products. This support includes material selection guidance based on end-use conditions such as temperature ranges, exposure duration, mechanical stress, and cleaning requirements. Engineers conduct compatibility testing to ensure membranes bond properly with adhesives, sealants, and other materials in your assembly process. They also provide processing recommendations covering storage conditions, handling procedures, cutting methods, and application techniques that maximize membrane performance and minimize waste. Many factories offer prototype development services where they produce small quantities of customized membranes for your testing and evaluation before committing to full production runs. This collaborative approach reduces development time, prevents costly mistakes from inappropriate material selection, and accelerates your path from concept to market-ready products. The application engineering relationship often includes ongoing support as products evolve or enter new markets with different requirements, creating a partnership that supports long-term business growth rather than transactional material purchases.
Rigorous Quality Assurance and Certification

Rigorous Quality Assurance and Certification

A professional waterproof breathable membrane factory maintains rigorous quality assurance protocols and industry certifications that provide assurance and simplify your compliance requirements. Comprehensive testing laboratories within the factory perform standardized evaluations including hydrostatic pressure resistance, moisture vapor transmission rates, tear strength, tensile properties, and accelerated aging studies. These facilities typically hold ISO 9001 quality management certification alongside product-specific certifications relevant to target industries such as construction, medical, or outdoor equipment sectors. Documentation systems track raw material sources, production parameters, and test results for complete traceability from incoming materials through finished goods. This documentation becomes invaluable when you need to demonstrate compliance with building codes, safety regulations, or customer specifications. Regular third-party audits verify that factory operations maintain certified standards and follow documented procedures consistently. Quality assurance extends to packaging and shipping processes that protect membrane properties during transportation and storage. For customers, this systematic quality approach means receiving materials with verified performance characteristics, comprehensive technical data sheets, and certification documentation that streamlines your own quality processes and regulatory submissions, ultimately reducing time and costs associated with material validation and compliance verification.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000